Workshop Equipment
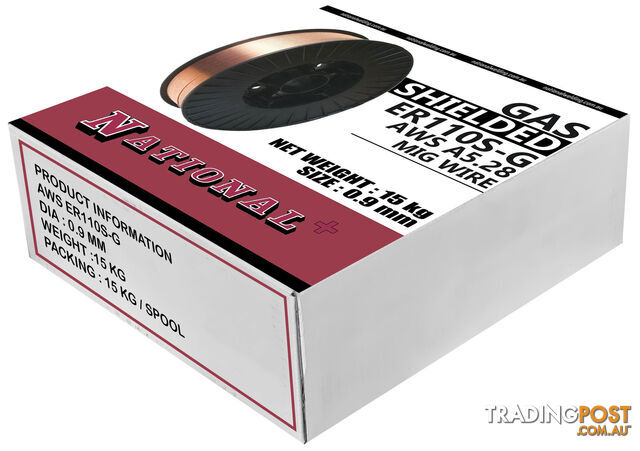
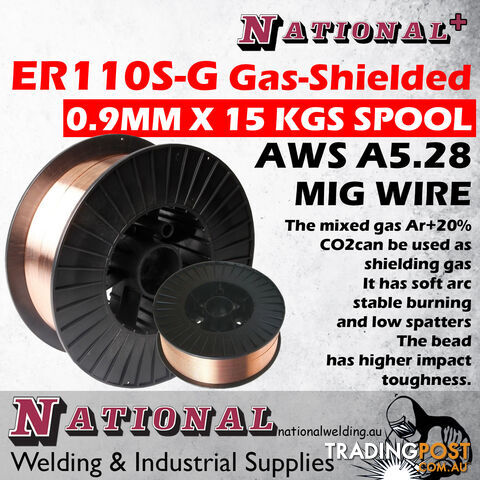
0.9mm 15Kgs Spool Gas-Shielded AWS A5.28 ER 110S-G Welding Wire 110S-G09
 +2 photos
$220
Verified seller
Description
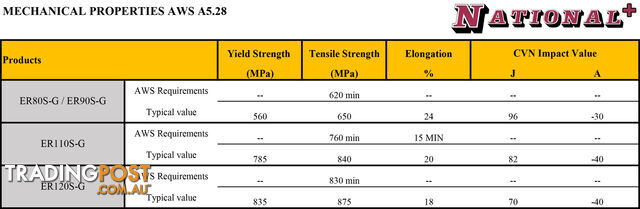
Use with 5-25% CO2/ Ar mixed shielding gas. Capable of producing welds with 760 MPa tensile strength & high impact values at -40. Designed to be used in applications such as crane manufacturing &offshore.
Advantages
Excellent weldability - Stable arc, low spatter, low clean up, suitable for both short-circuit transfer and high current spray transfer.
Superb feedability - Unique manufacturing technology results in a clean wire surface, smooth copper coating layer and an even amount of feeding lubricant. These advantages ensure lower friction during wire feeding and better electrical conductivity
AWS A5.28 ER110S-G
MIG welding wire AWS A5.28 ER110S-G,is a kind of high strength gas-shielded welding wire. The mixed gas Ar+20% CO2 can be used as shielding gas. It has soft arc, stable burning and low spatters. The bead has higher impact toughness.
Features:
Copper Coated, Low Allloy Gas Metal Arc (MIG) Welding Wire.
All Positional Welding of Medium and High Strength Steels
Welded Strength 760 MPa Tensile Class
Classification:
AS/NZS 16834-B G 78A 4U M21 G
AWS A5.28 ER110S-G
Description & Applications:
Austmig NiCrMo is a copper coated, low alloy solid wire suitable for the all positional welding of high strength steels using Argon + CO2 gas mixtures.
Austmig NiCrMo is ideal for the full strength welding of quenched and tempered structural steels, of the 760 MPa tensile class, such as USS-T1, CcMo Pipe, Welten 80, Weldox 700, X80, N-A-XTRA and Bisplate 80.
Operational Data:
Wire Size (mm) - 0.9mm
Welding Current Range (A) - 120 - 350
Arc Voltage Range *(V) - 18 - 32
Welding Current DC +
*Voltage is determined by arc current and electrode arc length. Welding currents and voltage shown are operational guides only.
NOTE: Austmig NiCrMo is NOT to be used in weldments which are to be stress relieved.
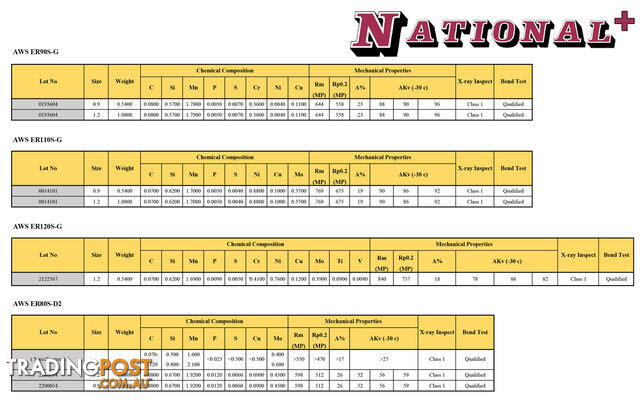
Typical All Weld Metal Chemical Analysis:
C - 0.08
Mn - 1.60
Si - 0.60
Ni - 1.50
Cr - 0.30
Mo - 0.30
V - 0.10
Typical All Weld Metal Mechanical Analysis:
Gas Type - Ar+18% CO 2
Yield Stress - 750 MPa
Tensile Strength - 800 MPa
Elongation - 19%
CVN Impact Values - 70J @ -40ºC
In as welded condition.
NOTE: The use of less oxidizing argon based gas mixtures (ie Ar/O2 , Ar/CO2 , Ar/CO2 /O2 ), will result in higher alloy recovery in the weld metal, leading to higher tensile properties.
Packing Data:
Wire - 0.9mm
Pack Size and Type - 15kg Spool
National Plus Guarantee
Quality Products at extraordinary rates. We choose from a range of dependable brands, that have proven that they can get the job done.
Our purchasing team negotiates with a variety of suppliers to deliver you quality products at affordable rates.
Seen a better price, or do you have any compliments or complaints? Contact us directly for after sales support and well work together to solve any problems.
Part Number/SKU: MW110SG09300
* Product Images are for illustration purposes only, unless otherwise specified colour may be different.
Location
Australia
Location is approximate - the map shows the general area, not the exact address.
$220
Stay safe: buyer safety tips
National Welding SuppliesVerifiedVerified Tradingpost seller
You may also like
 Workshop Equipment
$500$280 moreNegotiable
Stainless Steel Work Benches
 Workshop Equipment
$51.75$168 less
Fibre Disc 982C 180mm 36+ 3M™ Cubitron™ 7000028201 Pack of 5
 Workshop Equipment
$7.50$213 less
Flexible Grinding Wheel 125 x 3 x 22.23mm 60+ 3M 7012802925 (14444) Each
 Workshop Equipment
$346.90$127 more
Flexible Grinding Wheel 125 x 3 x 22.23mm 60+ 3M 7012802925 (14444) Pack of 50
 Workshop Equipment
$31$189 less
Fibre Disc Backup Pad 125mm Ribbed to Suit M14 - 2mm (5/8") Thread 7000105442 3M...
 Workshop Equipment
$24.75$195 less
Fibre Disc 982C 125mm 80+ 3M™ Cubitron™ II 7000028197 Pack of 5
 Workshop Equipment
$24.75$195 less
Fibre Disc 982C 125mm 60+ 3M™ Cubitron™ II 7000028195-5 Pack of 5
 Workshop Equipment
$37.30$183 less
Grinding Wheel Depressed Centre 230 x 7 x 22.23 mm 36+ T27 Cubitron™ III...
 Workshop Equipment
$25.40$195 less
Fibre Disc 982C 115mm 36+ 3M™ Cubitron™ II 7000028192 Pack of 5
 Workshop Equipment
$24.75$195 less
Fibre Disc 982C 100mm 80+ 3M™ Cubitron™ II 7010362292-5 Pack of 5
Message seller
About 0.9mm 15Kgs Spool Gas-Shielded AWS A5.28 ER 110S-G Welding Wire 110S-G09
Report this ad
Tell us what's wrong with this listing.